Modular construction quality depends on what happens between modules
A factory can deliver a well-made building module while the completed building still encounters problems at its connections. Recent research makes the boundary between factory production and site assembly an important place to examine modular construction claims.
As of November 15, 2025. The useful question for a developer is specific: how will this building's separate parts become one verified system? A module arrives with its own dimensions, materials, records and completed work. The foundations, neighbouring modules and services must match those assumptions. That creates a coordination task which a fast installation schedule alone cannot resolve. A research review published in the 2025 Modular and Offsite Construction proceedings on November 1 groups adoption barriers across technical, organizational and other areas. Its proposals are useful starting points, but the authors also call for a future stakeholder survey to validate and prioritize the barriers. It should be read as a structured review, rather than a measured ranking of the problems on every project.
Read the evidence before accepting the benefit
Modular construction covers different products and delivery arrangements. A bathroom pod, a structural panel and a fully enclosed room module do not move the same work into the factory. Comparing their performance without identifying the system can make a plausible benefit sound more universal than the evidence supports.
An earlier review by Alhawamdeh and Lee, first published in 2024, draws together barriers reported in offsite construction literature. Its categories include transport limitations, coordination and constraints on late design changes. The frequency with which researchers discuss a barrier is useful for identifying questions. It does not establish the probability that a particular building will suffer that problem.
For a proposed project, the next step is to translate a general finding into something observable. If coordination is the concern, ask for the drawing approval sequence and the procedure for resolving inconsistent dimensions. If late changes are the concern, identify the last practical decision date for each component. These are more useful responses than assigning a general risk score to the entire construction method.
The comparison with conventional construction also needs a consistent starting point. A modular schedule beginning after design approval should not be compared with a traditional schedule beginning at the first concept meeting. The same principle applies to defects: count equivalent stages and responsibilities, including repairs completed before delivery.
A handover is also a technical interface
UK research published in November 2024 examines potential safety and performance risks in volumetric construction. It highlights the transition from offsite manufacture to onsite installation, including tolerances, sequencing and understanding of the original design. The report was finalized in 2022 and explicitly says the evidence cannot establish how frequently the identified risks occur. It is a map of possible failure points, not a current defect-rate survey.
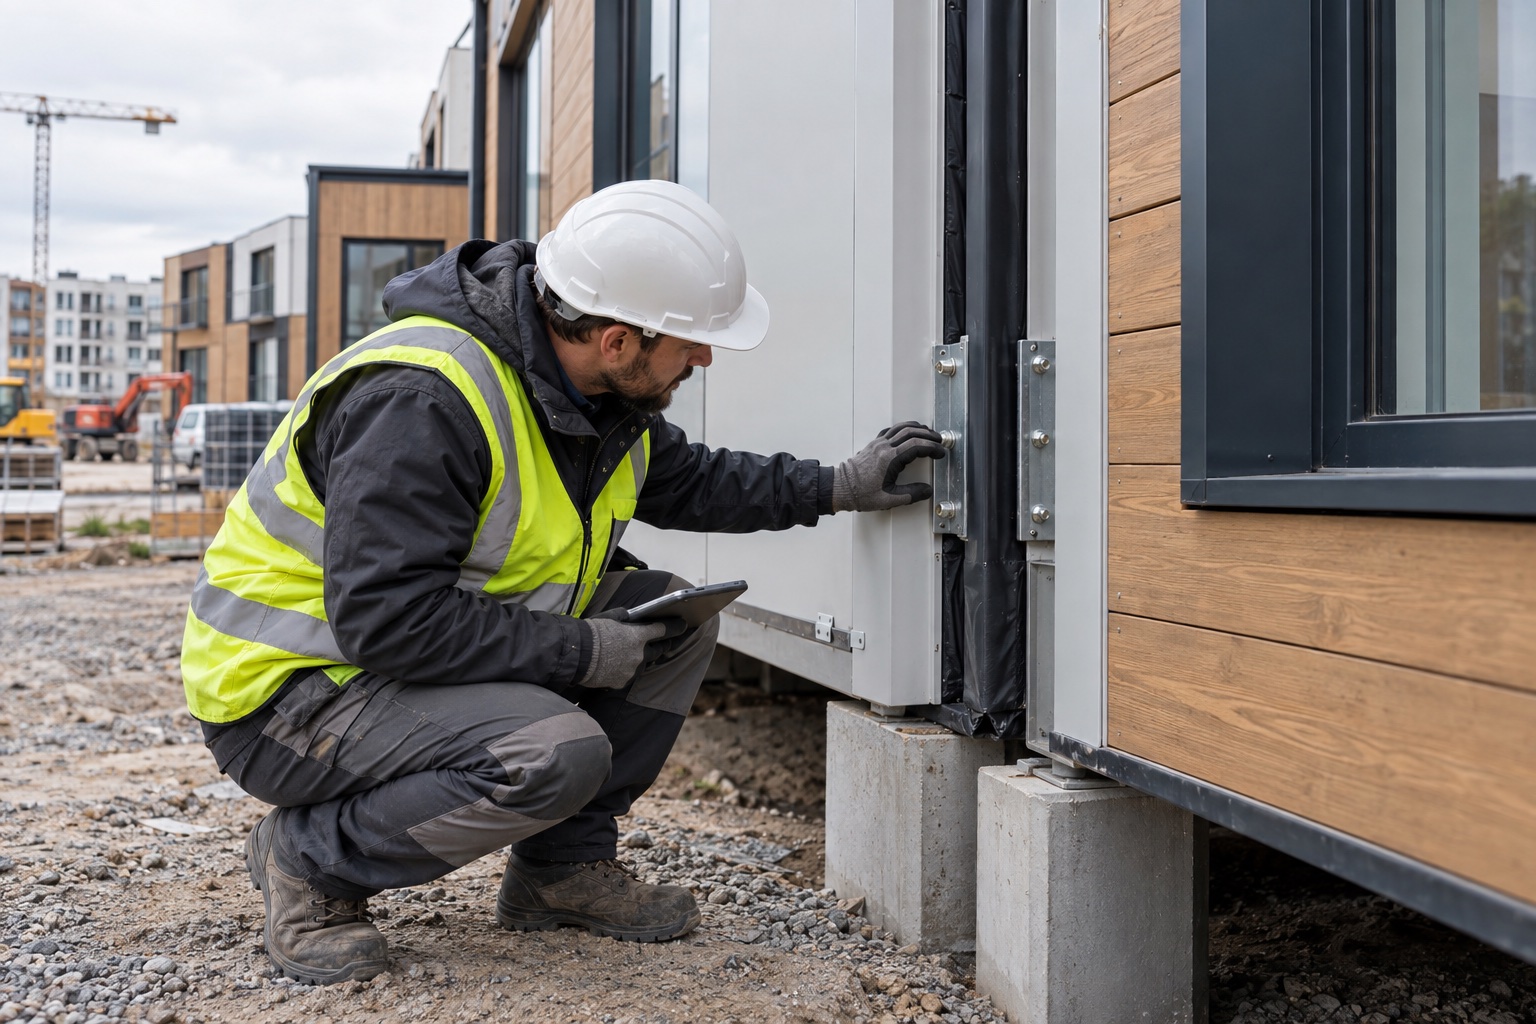
Consider an illustrative apartment project. The factory checks each module against an approved model. The site team surveys the foundation. Both checks can pass their separate acceptance criteria, yet a difference in the reference points used by the teams can create an assembly problem. The response is to reconcile the measurement system before dispatch, rather than assume that two inspection certificates establish compatibility.
The same reasoning applies to services. A pipe connection needs more than the correct nominal diameter. Its location, access space and installation sequence must work with the adjoining module. A detail that is easy to inspect on an open production line can become difficult to reach after neighbouring units are installed.
A practical interface register would therefore identify the connection, responsible parties, approved detail and verification stage. It should also state what happens when a measurement falls outside the agreed range. Without that decision path, crews may face pressure to improvise while expensive lifting equipment waits.
Design decisions need a release sequence
Singapore's Building and Construction Authority advises involving suppliers, manufacturers and the main contractor during PPVC design. That is useful background guidance for understanding why production knowledge belongs in early decisions. It is not a substitute for the requirements that apply in another jurisdiction.
For a project team, early involvement should produce visible outputs. Transport dimensions should inform the module design. Installation access should inform the connection detail. Inspection access should inform when finishes are closed. A coordination meeting has limited value if its decisions never reach the drawings used by the factory and installers.
There is also a distinction between freezing everything and controlling change. Some choices may remain flexible without affecting the structural or service interface. Others could require changes across many repeated modules. A release sequence helps the client understand which decisions are reversible, which create cost and which require renewed technical review.
Suppose a client changes a service location after fabrication begins. The relevant comparison is not simply the price of moving one outlet. The team should identify affected drawings, stock, completed modules, inspections and site connections. This illustrative exercise shows why the consequences of a change can extend well beyond the visible fitting.
A documented change should travel with the affected module. The site team needs to know which version was built, including approved departures. A drawing repository with many files is less useful than a reliable way of connecting one delivered unit to its actual configuration.
Inspection evidence should survive delivery
Factory inspection, dispatch acceptance and final installation acceptance answer different questions. Combining them into one general quality statement can obscure work that nobody has actually checked. A project-specific inspection plan should make their boundaries explicit.
A useful record might connect a module identifier with its inspection results, unresolved items and approved corrections. Site receipt can then check condition and configuration against that record. Installation verification can address the connections made after delivery. The value comes from continuity, rather than from the volume of photographs or forms collected.
Hidden work deserves particular attention. The project team should identify which details will become inaccessible and arrange appropriate verification before closure. The methods and acceptance criteria belong with the responsible designers and competent inspectors. A general article cannot prescribe one inspection approach for every system, material or building.
Transport and temporary storage should sit within the same chain of responsibility. If a unit arrives damaged or wet, the team needs a process for deciding whether remedial work is necessary and who approves it. The delivery receipt alone cannot determine whether concealed components remain fit for their intended use.
This approach also supports learning. When an installation problem occurs, the record should help distinguish design mismatch, manufacturing variation, transport damage and assembly error. Treating every correction as a generic site defect would hide information that could improve the next production run.
Measure the completed delivery system
HUD's earlier Offsite Construction for Housing research roadmap, posted in 2023, identifies research needs across system performance, contracts, workforce and business models. Its breadth is a useful reminder that industrializing housing involves more than the equipment inside a factory. A research agenda does not itself prove that any particular delivery model will succeed.
For buyers, a balanced assessment should follow the building through completion. Useful measures could include first-time acceptance at defined stages, unresolved interface issues, rework hours and the time taken to close defects. Each measure needs a clear definition so that factory and site work remain comparable.
Commercial arrangements should support those measures. If separate packages reward factory dispatch and site installation without a shared completion requirement, the client should examine who owns the unresolved boundary between them. This is a question for project procurement and professional review, not a claim that one contract form suits all modular buildings.
The strongest proposal will explain how the building can be verified after its parts have come together. It will show the approved interfaces, the evidence retained through delivery and the route for resolving deviations. Factory production can change where work happens. Confidence in the finished building depends on keeping design intent and accountability intact across that entire journey.
Source: Azarian et al. MOC review; Alhawamdeh and Lee; MHCLG; HUD; BCA · Cover: AI-generated illustration